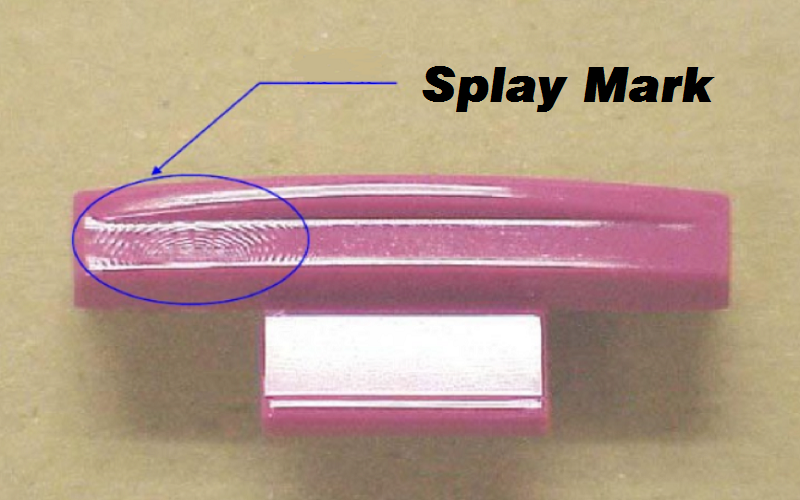
In the plastic injection molding industry, manufacturers and process engineers frequently encounter the surface defect known as “splay.”
This injection molding defect characterized by silvery streaks or spots on plastic components, not only diminishes the visual appeal but can also compromise product performance and quality.
This article is specifically designed for injection molding professionals seeking to understand the root causes of splay, explore practical solutions, and implement effective prevention strategies.
By gaining insight into how splay forms and how to control it, these stakeholders can enhance production efficiency and ensure their molded parts meet stringent quality standards.
What Is Splay In Injection Molding?
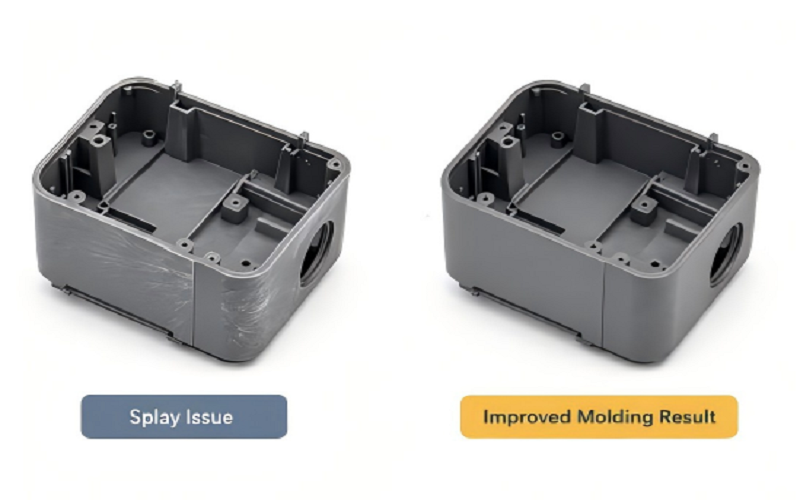
Splay is a surface defect in plastic injection molding characterized by silvery streaks, lines, or spots that appear on the surface of molded parts. These marks are often referred to as silver streaks or splay marks and are considered a cosmetic defect that can detract from the visual appeal of the finished part.
Beyond aesthetics, splay can also indicate underlying issues in the injection molding process that may affect the structural integrity and performance of the molded parts.
Splay typically occurs when volatile gases, moisture, or trapped air within the polymer melt are forced to the surface during the injection molding process. These gases expand rapidly as the molten plastic fills the mold cavity, creating the characteristic silvery or cloudy streaks.
The defect is most commonly seen in hygroscopic plastics, such as polycarbonate and nylon, which absorb moisture from the environment if not properly dried before processing.
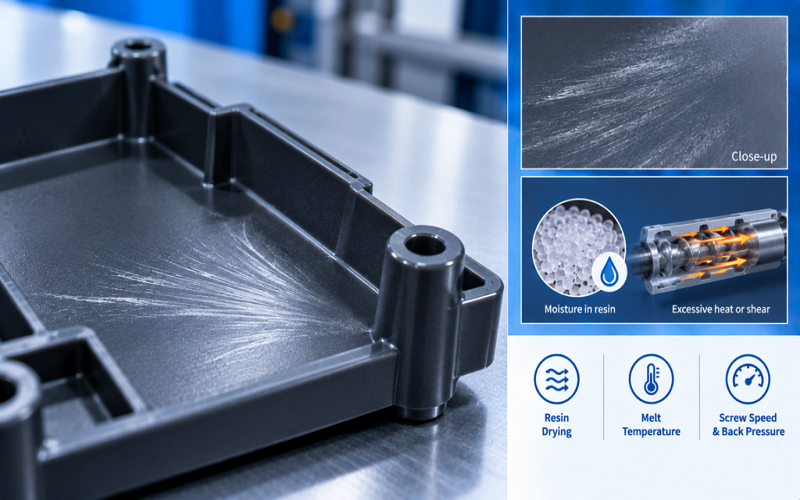
What Causes Injection Molding Splay?
Injection molding splay can be caused by several factors related to the material, machine settings, mold design, and processing conditions. Understanding these causes is essential to effectively prevent and fix splay issues.
1. Material-Related Causes
Excessive Moisture Content
One of the most common causes of splay is excessive moisture in the resin. Hygroscopic resins such as polycarbonate (PC), nylon (PA), and ABS absorb moisture from the environment. The presence of moisture leads to steam formation at high temperatures, causing splay defects.
Improper Drying
If the resin is not adequately dried or the dryer temperature is set improperly, moisture vaporizes during the injection molding process, forming steam bubbles that appear as silver streaks on the molded part surface. Improper drying material that is not completely dry is often the root cause of splay.
Excessive Heat
Excessive barrel temperature, overheating of heater bands, or improper barrel temperature settings can all lead to degradation of polymer chains. Too much heat in the feed zone causes the plastic to melt too quickly, filling the runner and blocking the vent.
2. Improper Processing Conditions
High Injection Speed
High injection speed generates strong shear forces, which can cause localized overheating of the melt or air entrapment, leading to shear-type splay. Too fast injection speed also causes turbulent flow, making it difficult for air to escape and increasing the likelihood of splay.
Improper Back Pressure Setting
Low back pressure prevents effective venting of gases from the barrel, trapping air and bubbles in the melt and causing splay. Excessive back pressure can increase shear heat, resulting in material degradation and splay.
Excessive screw rotation speed
Excessive screw speed increases shear stress and heat, causing polymer chain breakage and material degradation, which in turn causes splay defects. Proper control of screw speed and rotation helps reduce shear heat and material degradation, maintaining melt quality.
Inconsistent Mold Temperature and Barrel Temperature
High barrel temperature causes material overheating and degradation, producing volatile gases that cause splay. Low mold temperature causes premature cooling of the melt, increasing flow resistance and shear stress, which can also lead to splay.
3. Mold Design Issues
Poor Mold Gate Design
The design of the mold gate directly affects melt flow and shear stress. Narrow or uneven gates restrict melt flow, causing localized high shear and increasing the risk of splay.
Inadequate Mold Venting and Exhaust
Insufficient mold venting traps air and gases inside the mold, causing splay. Lack of effective venting slots or vents in mold design prevents air from escaping smoothly, resulting in gas bubbles in the melt that show as silver streaks on the molded surface.
Solving splay problems requires a systematic approach combining adjustments in materials, equipment, and process parameters.
By monitoring and optimizing barrel temperature, mold temperature, injection speed, back pressure, screw speed, and drying conditions, splay formation can be effectively controlled, improving the quality of plastic injection molded parts.
Silver Streak Characteristics | Primary Suspected Cause |
|---|---|
Random location, uneven distribution | Moisture issue |
Fixed location, recurring appearance | Shear or mold-related issue |
Accompanied by darkening color or burnt smell | Material overheating and degradation |
Prominent near the gate | High injection speed or undersized gate |
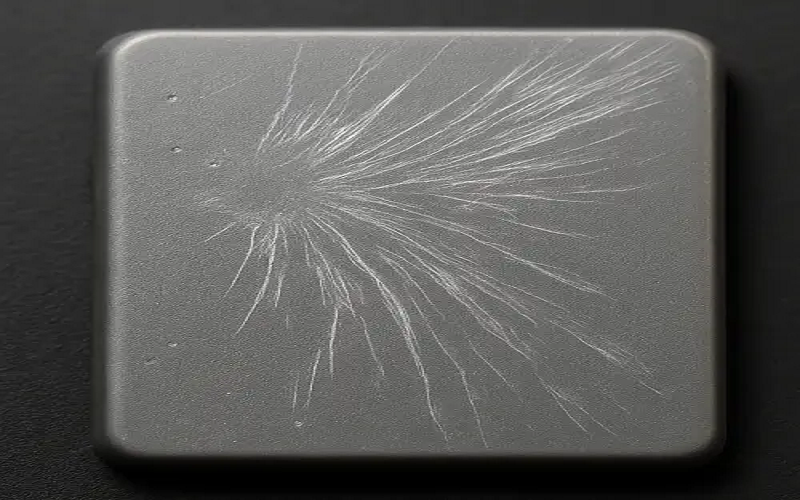
The Effect Of Splay In Injection Molding
Splay defects in injection molding have significant implications beyond just surface appearance. The presence of silvery streaks or lines on molded parts can lead to several negative outcomes affecting both the manufacturing process and the final product.
Impact on Final Product Quality
Splay marks often indicate underlying issues such as trapped gases, moisture, or polymer degradation. These defects can compromise the structural integrity of the molded parts, making them more brittle and prone to failure under mechanical stress.
As a result, the final product may not meet the highest quality standards required for critical applications.
Increased Scrap And Rework Rates
Parts exhibiting splay are frequently rejected during quality inspections due to their poor aesthetics and potential functional weaknesses. This rejection leads to increased scrap rates, wasting raw materials and increasing production costs.
In some cases, additional rework or secondary finishing processes may be necessary to salvage affected parts, further adding to manufacturing time and expenses.
Production Efficiency And Cost Implications
Splay defects often necessitate troubleshooting and process adjustments, which can cause downtime and reduce overall production efficiency.
The need to identify and correct the root causes—such as optimizing injection molding machines settings, improving drying procedures, or modifying mold design—can delay production schedules and increase operational costs.
Understanding and controlling splay in injection molding is crucial not only for maintaining the visual appeal of parts but also for ensuring their performance, reliability, and compliance with quality standards. Proactively addressing splay helps minimize waste, reduce costs, and improve overall production outcomes.
How To Fix Splay Injection Molding Issues?
Fixing splay issues in injection molding involves a systematic approach to identify and address the root causes. Below are proven steps and best practices to effectively reduce or eliminate splay defects:
1. Verify and Improve Material Drying
Proper drying of hygroscopic resins is critical. Use desiccant dryers set to the resin manufacturer’s recommended temperature and drying time to ensure moisture content is below 0.02%. Regularly check moisture levels with a moisture analyzer to confirm resin dryness before processing.
2. Adjust Injection Speed and Shear Rates
Reduce injection speed to lower shear forces and allow trapped air to escape more easily. Adjust screw speed and back pressure to minimize excessive shear heating that can degrade the polymer chains and cause volatile gases.
3. Optimize Barrel and Mold Temperatures
Maintain barrel temperatures within the recommended range to prevent overheating. Lower feed zone temperature if necessary to reduce material degradation. Ensure mold temperature is optimized to prevent premature cooling and high shear at the melt front.
4. Improve Mold Venting and Design
Enhance mold venting by adding or enlarging vents to allow trapped air and gases to escape efficiently. Evaluate and optimize gate design to reduce flow restrictions and shear stress during injection. Ensure runners, gates, and nozzles are free from obstructions.
5. Control Back Pressure and Screw Rotation
Set back pressure to an optimal level that prevents air entrapment without causing excessive shear heat. Reduce screw rotation speed to limit shear stress and material degradation during plasticizing.
By following these steps and continuously monitoring the injection molding process, manufacturers find the true source and determine the best course for addressing your unique situation.
Conclusion
Splay in injection molding is a common yet critical defect that impacts both the appearance and functionality of molded plastic parts. It primarily arises from moisture, trapped air, excessive heat, shear stress, and inadequate mold venting.
Understanding these root causes enables manufacturers to implement targeted prevention and corrective measures such as proper resin drying, optimized injection speed, controlled barrel and mold temperatures, improved mold venting, and precise machine settings.
By systematically addressing these factors, manufacturers can significantly reduce splay defects, enhance product quality, minimize scrap and rework, and improve overall production efficiency. To learn more about injection molding, please contact us.